

Belt conveyor transfer point design has a direct effect on product flow, spillage, dust, belt wear, cleanup time, and the reliability of the line after installation. A transfer point is not just the place where one conveyor drops onto another. It is the controlled handoff between product, belt, chute, skirt sealing, supports, guarding, access, and the next process.
This guide is written for plant engineers, project buyers, maintenance teams, and operations managers preparing a conveyor RFQ or reviewing an existing transfer problem. It does not assume a specific product, belt width, plant output, chute material, motor size, or certification. The goal is to help buyers describe the real operating conditions clearly so suppliers can design a cleaner and more serviceable transfer.
Why Transfer Points Decide Conveyor Cleanliness
A conveyor can have the right belt, motor, pulleys, and controls but still create daily cleanup if the product enters the receiving belt poorly. When material lands off center, at the wrong angle, from too much height, or with uncontrolled impact, it can bounce, slide, spill, and push the belt toward one side. The visible symptom may be material on the floor, but the root cause is often transfer geometry.
Clean product flow starts with how the material leaves the upstream equipment and how it meets the receiving conveyor. That handoff should match the product size, flow rate, fragility, moisture, dust level, and required belt speed. It also needs enough access for inspection and cleaning, not just enough space for the equipment to fit on the drawing.
Start With the Product and Flow Path
The first design question is simple: what exactly is moving through the transfer? Boxes, bags, parcels, bakery trays, bottles, loose parts, grains, pellets, powders, and metal stampings all behave differently. A smooth sealed chute for one product may damage another product or create a blockage in a different plant.
Before comparing quotes, define the product size range, weight range, surface condition, moisture, temperature, dust level, breakage risk, and normal flow rate. If the product mix changes by shift or season, include that range as well. A transfer designed only around the average product can fail when the smallest item catches a gap or the largest item strikes a guide.
Control Drop Height and Entry Angle
Drop height controls impact energy. A high drop may cause product bounce, belt cover damage, noise, dust release, and faster wear at the loading zone. The best transfer is usually not the one with the shortest equipment footprint. It is the one that lets the product land in a controlled way while preserving the required throughput.
Entry angle matters as much as height. Product should arrive in a direction that supports belt travel, not fight it. A side-loaded transfer can work, but it must be designed intentionally with guides, chute geometry, belt support, and enough settling distance. If product repeatedly lands off center, the transfer may contribute to conveyor belt tracking problems even when the belt and pulleys are otherwise acceptable.
Center the Load Before It Becomes a Belt Problem
A receiving conveyor is easier to keep clean when the product lands near the intended centerline. Off-center loading can overload one side of the belt, press product into the skirt area, create uneven dust patterns, and increase edge wear. On parcel, tote, or carton lines, off-center loading can also create skewed product orientation that affects downstream scanning, sorting, or accumulation.
For new systems, compare the transfer centerline with the complete conveyor layout drawing. Look for product direction, elevation change, approach angle, maintenance clearance, and whether an operator can see the loading point safely. A drawing that shows only conveyor rectangles may not be enough to confirm product behavior.
Support the Belt Through the Loading Zone
The belt needs stable support where product lands. If the receiving belt sags between rollers, product can trap in gaps, skirt seals can lose contact, and impact can accelerate belt damage. Support details may include closely spaced idlers, impact rollers, slider beds, cradles, or other application-specific support methods.
When reviewing belt conveyor rollers, support beds, and conveyor pulleys, ask how the loading zone handles impact, belt sag, cleaning, and replacement access. The design should protect the belt without creating a service task that requires dismantling half of the transfer structure.
| Transfer design factor | What it affects | Useful RFQ detail |
|---|---|---|
| Product entry angle | Centering, bounce, skew, and belt loading | Show upstream and downstream flow direction |
| Drop height | Impact, dust, noise, and product damage | Provide elevation difference and product fragility |
| Belt support | Sag, skirt sealing, and belt cover wear | Note belt width, load weight, and impact point |
| Skirt and chute fit | Spillage, dust escape, and cleanup time | Describe dust level and cleaning method |
| Inspection access | Maintenance speed and safe troubleshooting | Share available side clearance and guard limits |
Use Skirting as a Seal, Not a Substitute for Bad Geometry
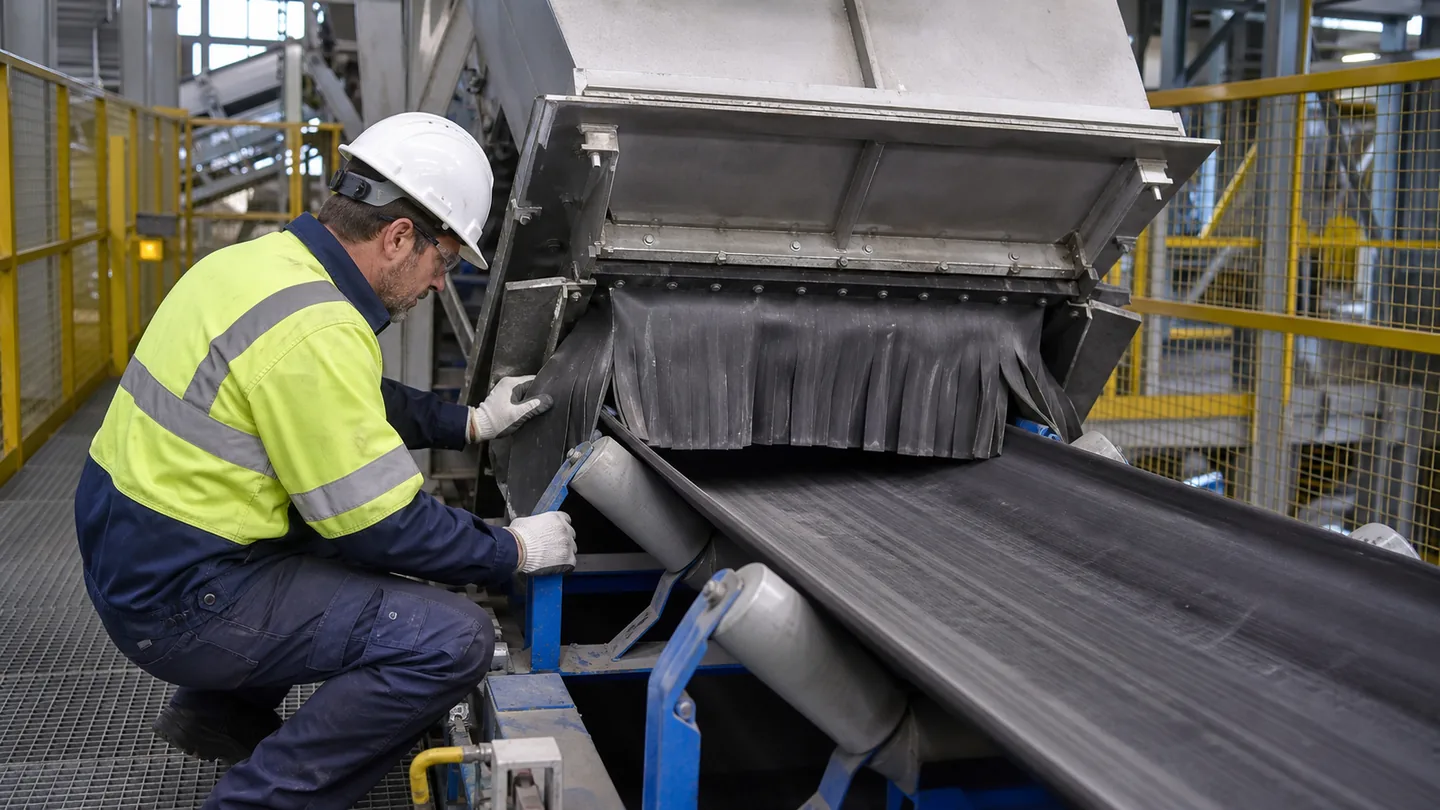
Skirt boards and seals help contain material at the loading zone, but they should not be asked to fix uncontrolled transfer geometry. If the product is entering with too much side force, too much bounce, or too much height, tighter skirting may only hide the problem while increasing friction, belt wear, and maintenance demand.
A good seal follows stable product flow. It should contain the normal material path, allow practical adjustment, and avoid rubbing harder than needed against the belt. For dusty or granular materials, the sealing approach should be matched with chute shape, belt support, and cleaning access. For packaged goods, guides should protect product orientation without pinching cartons or forcing items into a jam point.
Common Signs the Skirt Area Is Doing Too Much Work
Look for polished wear marks on one side, rubber dust near the seal, product buildup under the chute, frequent manual cleaning, recurring belt edge damage, or operators adjusting guides to compensate for product drift. These signs do not automatically prove the transfer is wrong, but they should trigger a review before another set of replacement seals is ordered.
Plan for Dust, Fines, and Product Carryback
Fine material changes the transfer design. Dust and small particles can escape through tiny gaps, collect around bearings, contaminate nearby equipment, or create housekeeping work that was not included in the original cost comparison. Carryback on the belt can also return material to unexpected areas, especially near pulleys and return rollers.
For dusty applications, describe the particle size, moisture, cleaning method, operating hours, and whether dust collection or enclosure is expected. Do not state that the conveyor must be dust-free unless the plant has defined what that means. A practical RFQ should explain the required level of containment and the inspection points needed to keep the system working.
Connect Transfer Design With Throughput
Throughput is not only a belt speed calculation. A transfer point must handle the actual arrival pattern of the product. A line may average the required rate but still overload the transfer in short surges. Accumulated cartons, irregular bag spacing, or batch discharge from upstream equipment can create a peak condition that is more important than the hourly average.
Use a practical conveyor throughput calculation to define the normal rate, peak rate, and product spacing. If the upstream conveyor releases items in groups, include that detail. For bulk flow, explain whether material arrives continuously, in batches, or from a controlled feeder. Suppliers need these details to size the loading zone and chute properly.
Make Maintenance Access Part of the Design
A clean transfer point still needs inspection. Guards, covers, chutes, sensors, and skirt assemblies should be arranged so maintenance teams can see wear points and clean safely. If the only way to inspect the transfer is to remove several guards in a cramped area, the plant may delay maintenance until spillage becomes obvious.
Access should be reviewed with the same seriousness as the drive, belt, and frame. Connect the transfer discussion with broader conveyor system components, because the chute, frame, belt support, bearings, guards, sensors, and cleaning points all affect the real ownership cost of the system.
What Operators Should Be Able to Check
Operators or maintenance staff should be able to observe product landing position, skirt condition, belt support condition, buildup, belt edge clearance, guard condition, and any visible dust escape. The required access depends on plant safety rules, but the design should not assume that hidden transfer points will stay clean without routine checks.
Do Not Ignore Controls and Product Detection
Mechanical design gets most of the attention, but controls can affect transfer cleanliness. Poor timing between conveyors can create product crowding, hard impacts, or gaps that disturb flow. Sensors placed too close to the transfer may become dirty or may not see skewed products consistently.
For packaged products, define whether the transfer needs product spacing, metering, accumulation control, or integration with downstream equipment. For bulk or loose material, describe any feeder, gate, diverter, or stop-start behavior that changes flow into the receiving belt. A transfer point is part of the process, not a passive gap between machines.
What to Include in a Transfer Point RFQ
A useful RFQ should include more than conveyor length and belt width. Provide product details, upstream equipment type, downstream equipment type, flow direction, elevation difference, target throughput, peak throughput, operating hours, cleaning method, dust or spillage concerns, available footprint, and photos or sketches of the current area if it is a retrofit.
For new lines, connect the transfer request with the full industrial conveyor system design discussion so the supplier can understand layout, product path, access, controls, and installation constraints together. For replacement or retrofit work, include a short note explaining what problem the current transfer creates and how often it affects production.
Simple RFQ Checklist
Before sending the request, collect product dimensions, weight range, flow rate, peak condition, upstream discharge height, receiving belt width, current spillage location, cleaning frequency, available side clearance, photos of the loading zone, and the shutdown window for installation. If the transfer affects downstream equipment, include that equipment in the photo set as well.
When a Retrofit Is Enough and When Redesign Is Better
Some transfer problems can be improved with better guides, skirt adjustment, belt support, chute liners, or access changes. Others need a larger redesign because the product is entering from the wrong height, angle, or speed. Replacing wear parts repeatedly may be cheaper in the short term, but it can be expensive if it does not remove the cause of spillage.
If the conveyor is old, overloaded, hard to clean, or no longer matched to the product mix, ask whether a redesigned section is more practical than another repair. A supplier should be able to explain what is being corrected and what operating details still need confirmation before quoting.
Final Takeaway
Cleaner conveyor flow depends on transfer point design as much as it depends on the belt itself. Control the drop, center the load, support the belt, match skirting to stable geometry, plan for dust and carryback, and give maintenance teams practical access. These details reduce cleanup work and make the conveyor easier to operate after installation.
If you are planning a new belt conveyor, troubleshooting a messy loading zone, or preparing a transfer retrofit, collect the product, layout, throughput, and access details before requesting a quote. ConveyorSolution can review those inputs and discuss a practical transfer approach for your application. Contact the team when you are ready to compare options or request an RFQ.
 French
 English
 Spanish
 German
 Portuguese
 Italian
 Russian